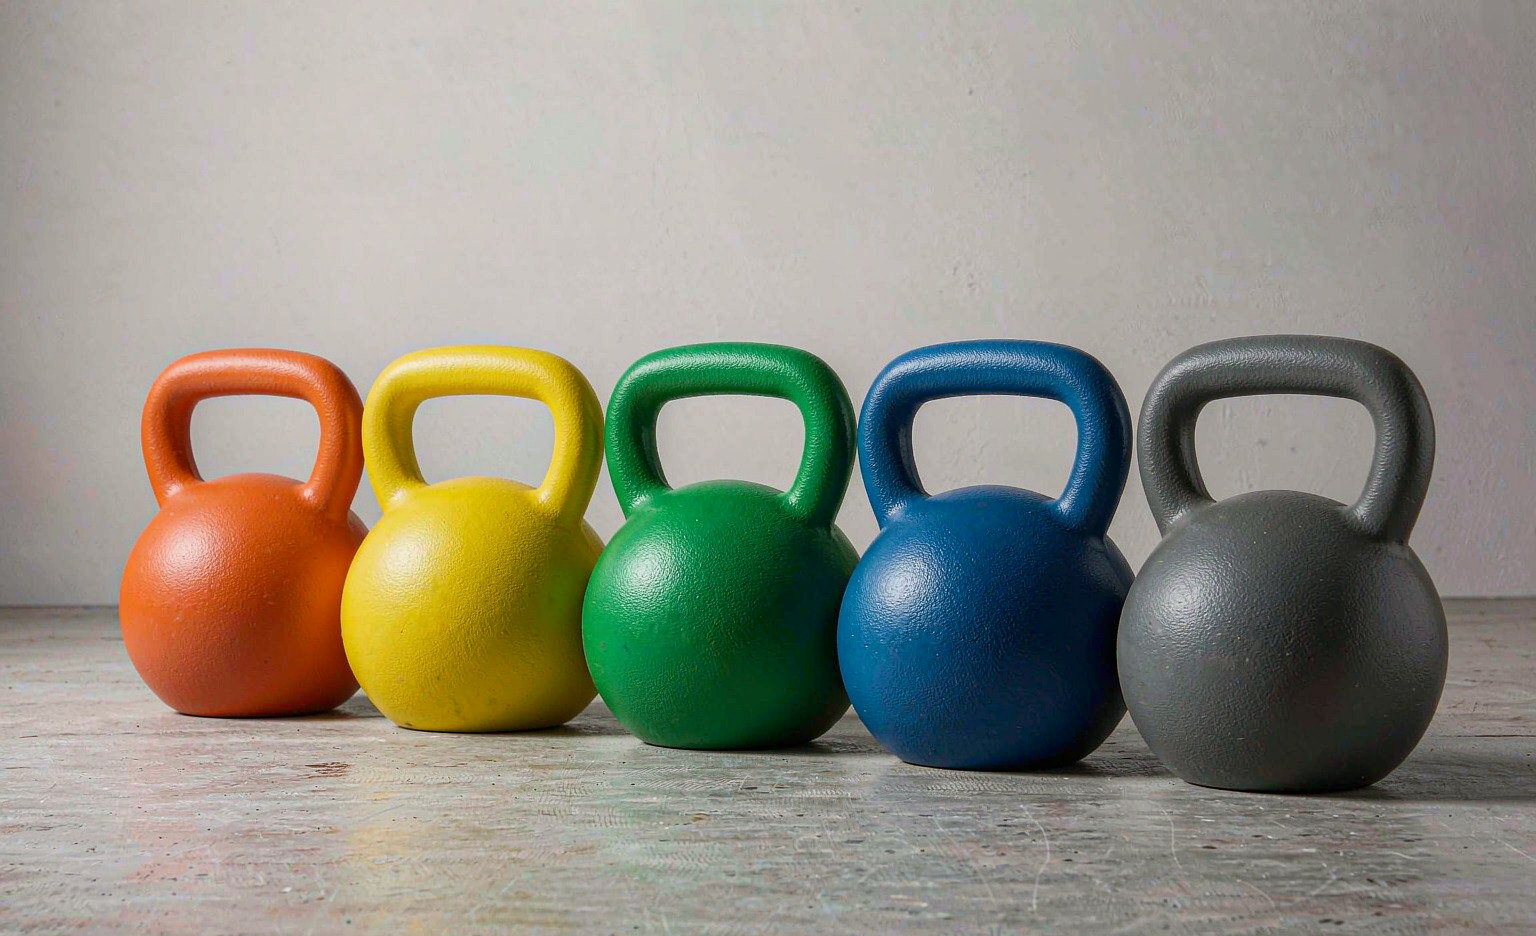Xianning, Hubei · Foundry + machining

One furnace.
Two businesses,
equal weight.

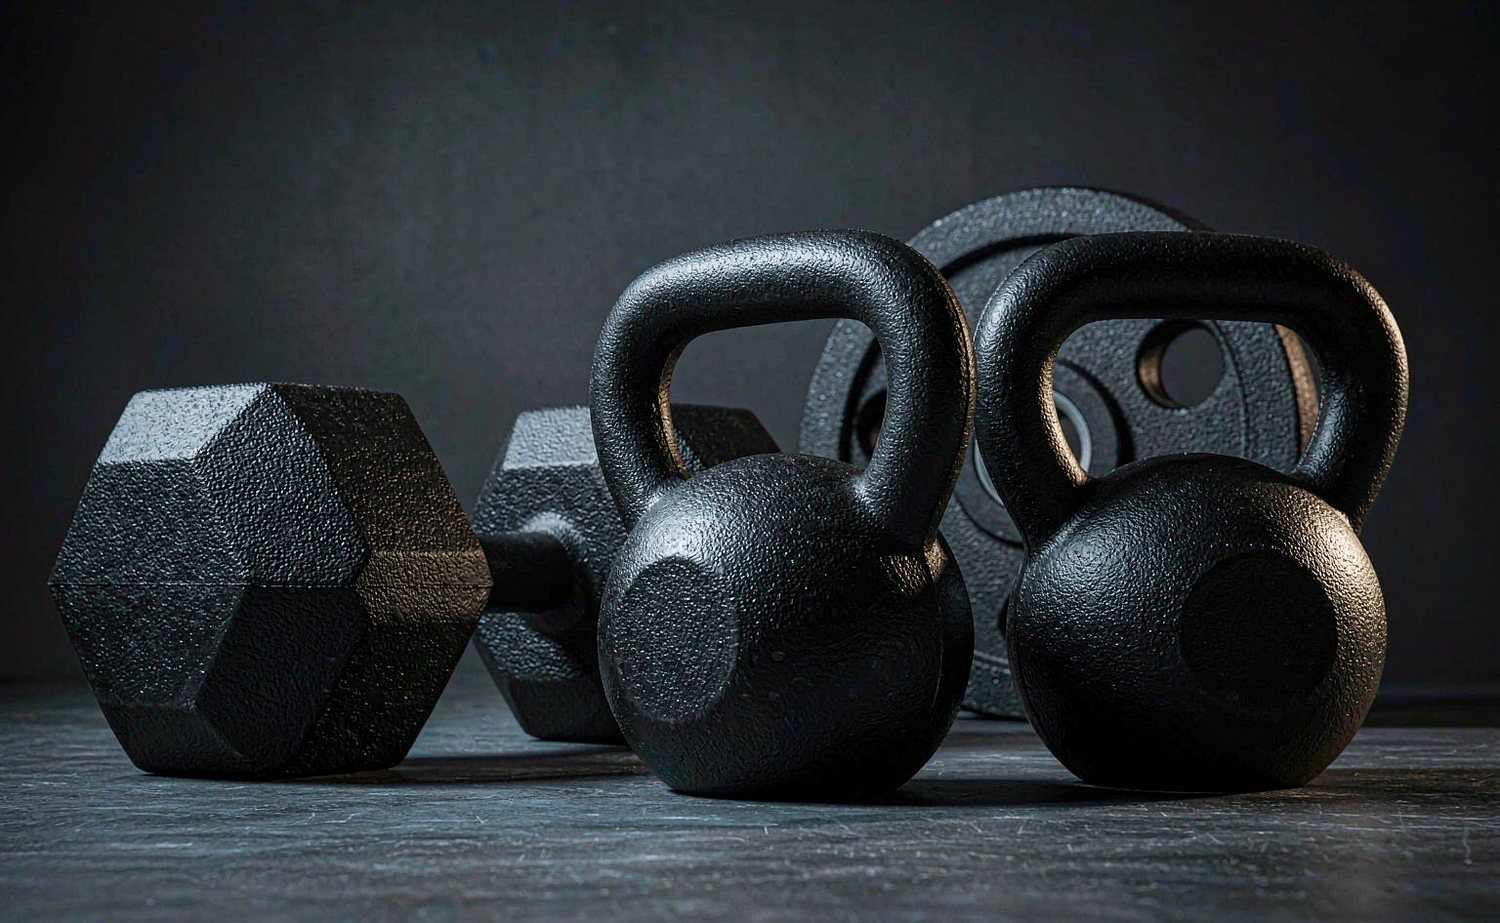
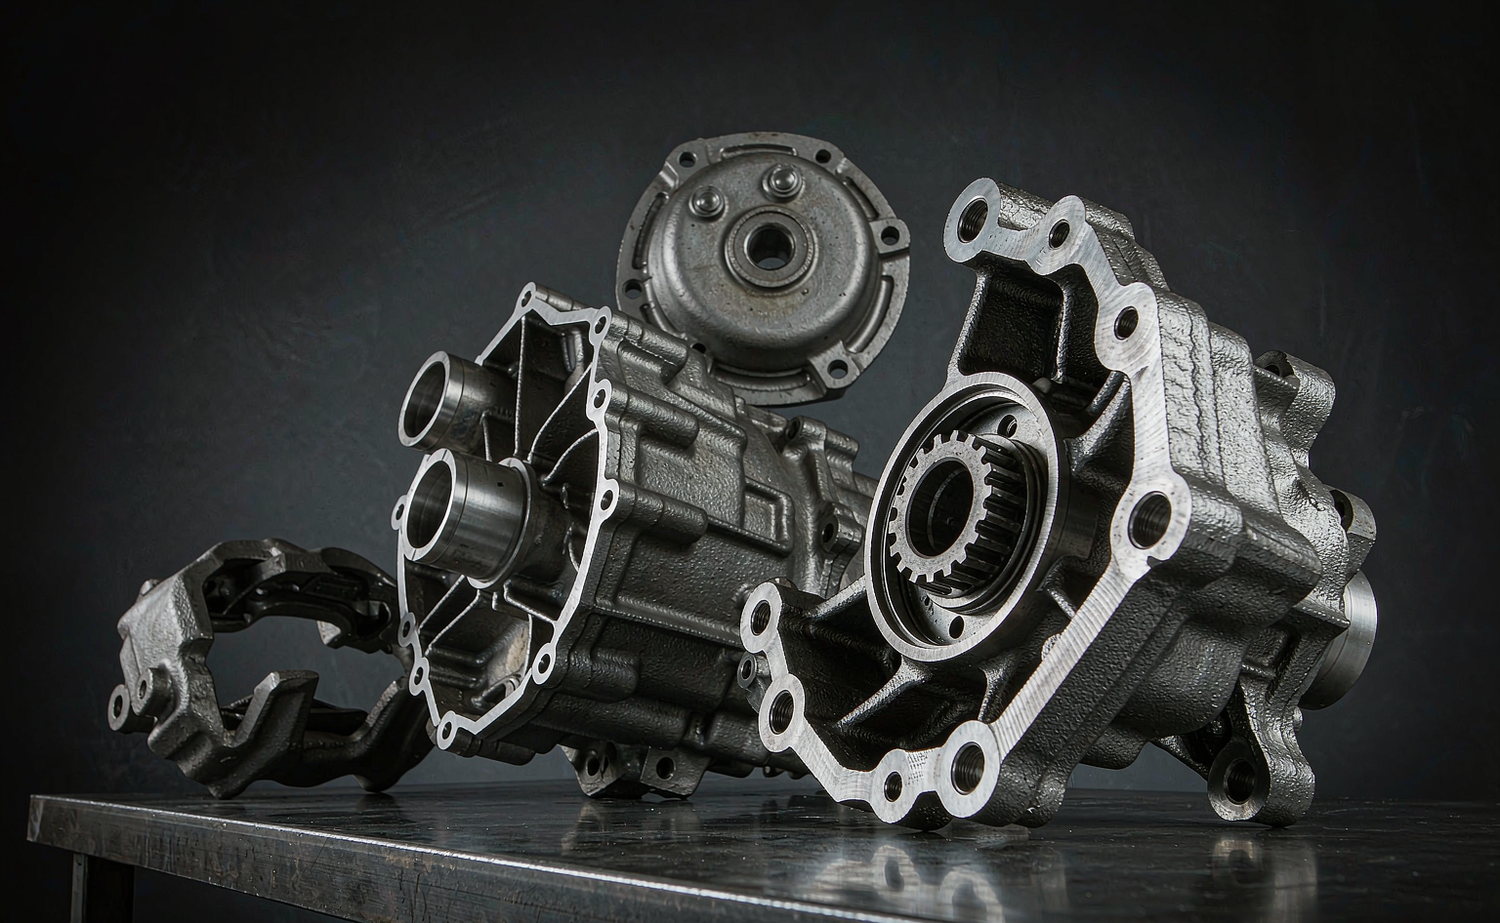
Cast-iron free weights and automotive castings leave the same floor, under the same heat record and the same first-article standard. Neither line is a side business — each has its own tooling, its own inspectors and its own buyers.

40,000m²Two plants, own land
260+65Foundry & machining units
±0.005mmBore tolerance, CMM checked
4–48kgKettlebell range, ±2% weight
Two product lines

Built to a model.
Or to your drawing.

A kettlebell buyer needs a fixed range, a stable price and a finish that repeats. An automotive buyer needs a first-article report and a heat number he can trace. Both are served from the same melt — by different tooling, different inspection plans and different people.

01 / Free weights

Built to a model number

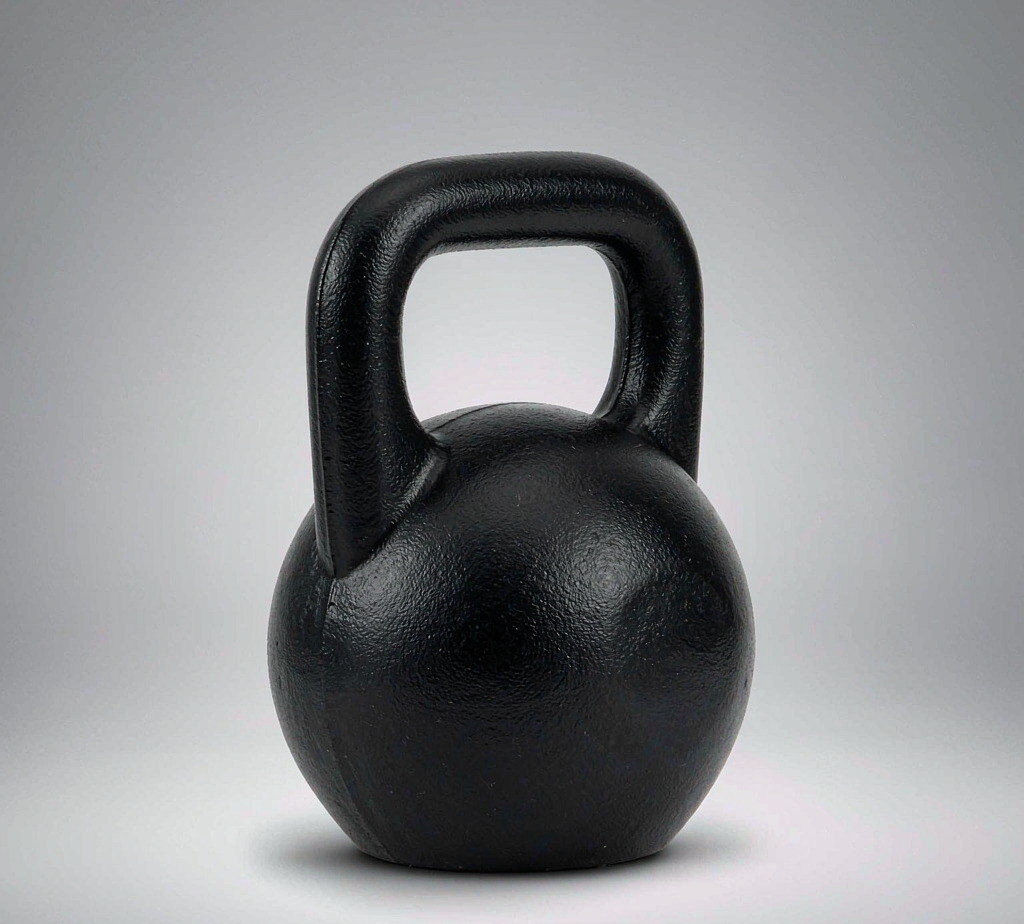
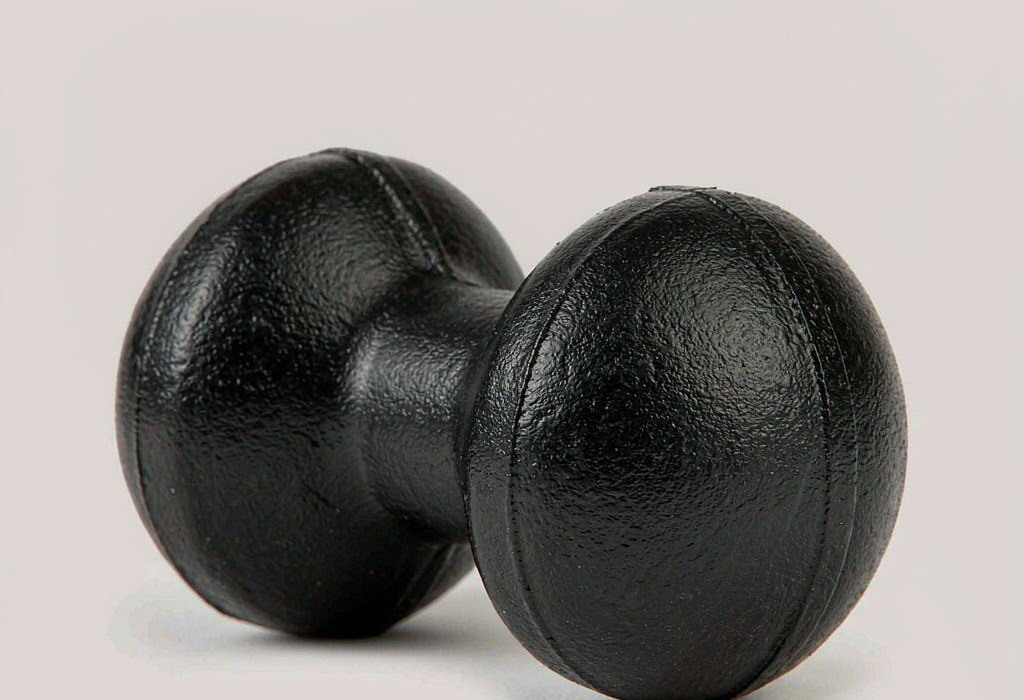
Kettlebells, dumbbells and plates in a range that repeats order after order. Competition kettlebells share one body size across the whole range, so a 12 kg and a 32 kg sit the same on the platform — only the core and the colour change.

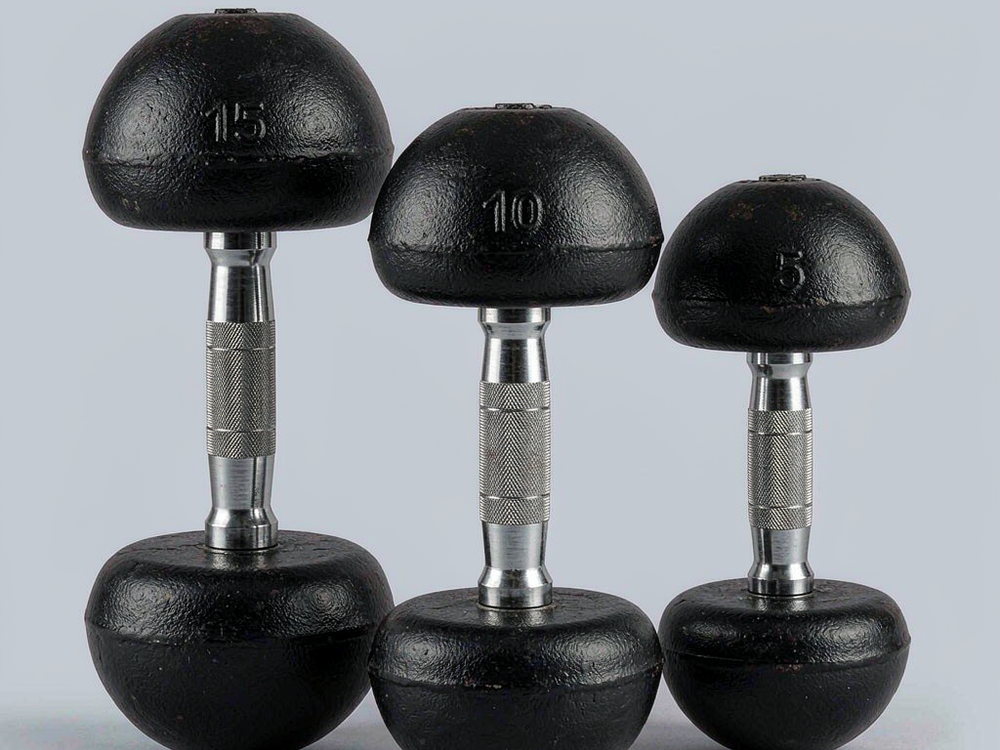
Single-piece cast iron kettlebell with a closed arch handle Three round-head cast iron dumbbells of increasing size in a row
Range
Kettlebells 4–48 kg · dumbbells 1–50 kg · plates 1.25–25 kg
Weight
±2% standard, ±1.5% competition — checked piece by piece
Finish
Powder coat, e-coat or urethane (partner line)
Branding
Logo cast into the body, colour code, kg or lb marking
Free weight specifications
02 / Automotive

Built to your drawing

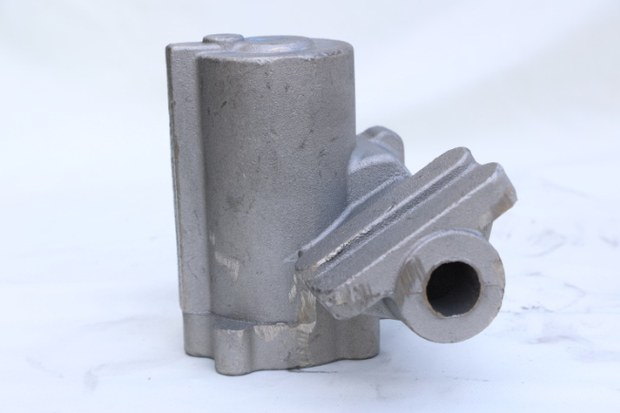
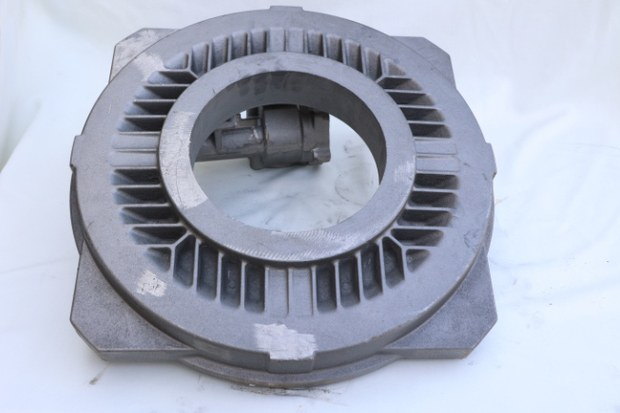
Steering housings, gearbox and reducer bodies, motor end covers, caliper brackets, valve and pump bodies, counterweights. Grey iron HT200–HT250 or ductile QT450-10, green-sand moulding with shell cores for the internal passages, then machined and measured in the second plant.

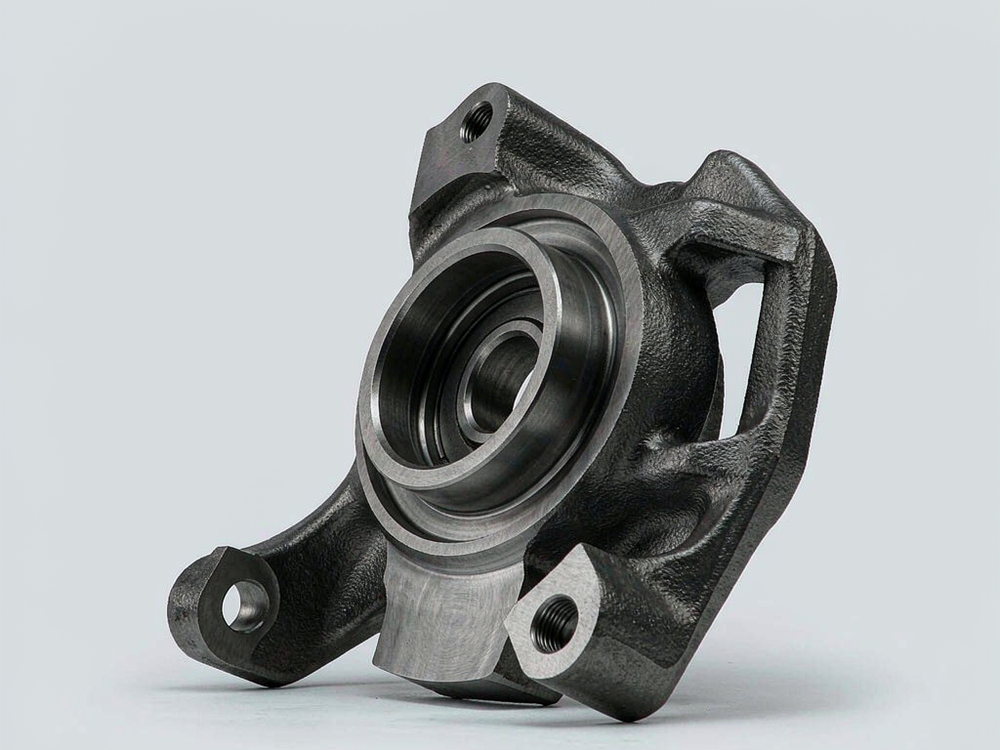
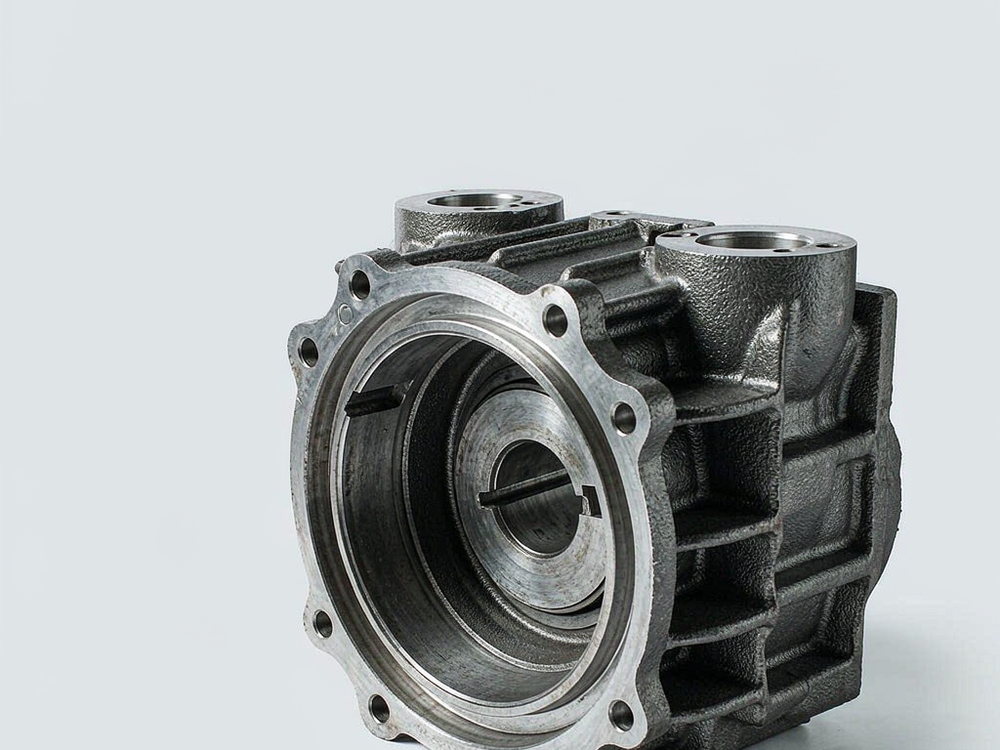
Ductile iron steering knuckle with machined hub bore and caliper mounting ears Grey iron gearbox housing with cooling ribs and a machined sealing flange
Material
HT200 / HT250 · QT450-10 / QT500-7, spectrum checked per heat
Moulding
Green sand on a DISA automatic line, shell cores for passages
Machining
Turn, mill, grind and CNC · bores held to ±0.005 mm
Documents
First-article report, CMM print, heat-number traceability
Casting capability
On the floor

Sixteen frames.
Two product lines.

Products, process close-ups and parts from current production. Filter by line — the point is that all of it starts at one furnace and leaves through one inspection room.

Classic cast iron kettlebell with a single-piece arch handle and matte black powder coat
Classic kettlebellSingle-piece sand casting · 4–48 kg
Gearbox housing casting with ribbed walls and a bright machined flange face
Gearbox housingGrey iron · machined sealing flange
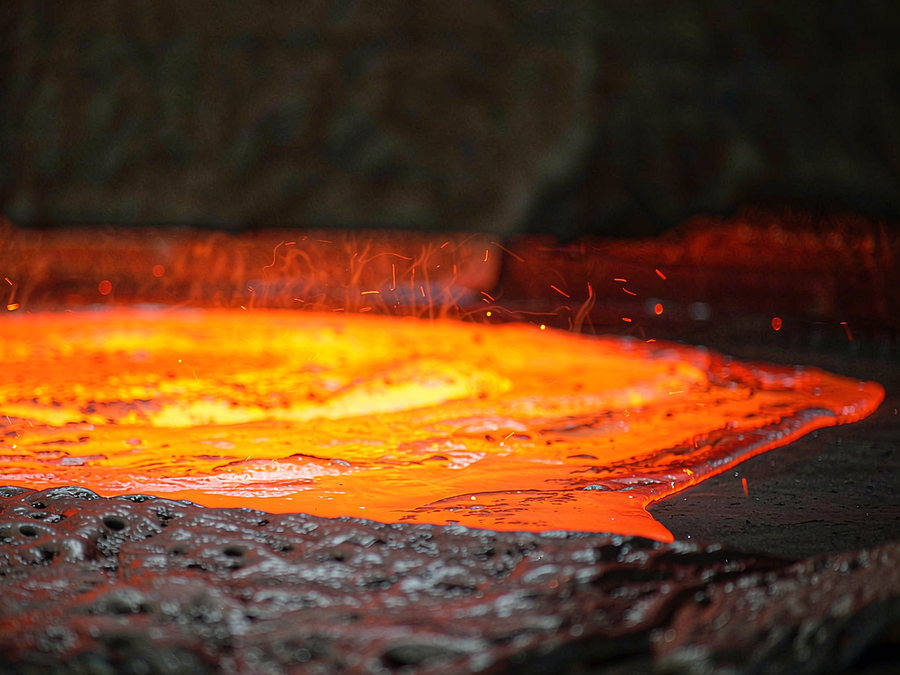
Surface of molten grey iron glowing orange in a foundry
Melt controlSpectrum analysis on every heat
Row of three round-head cast iron dumbbells with knurled steel handles
Round-head dumbbellsMatched set · 1–50 kg
Steering knuckle casting with central bearing bore and two caliper mounting ears
Steering knuckleDuctile iron · machined hub bore
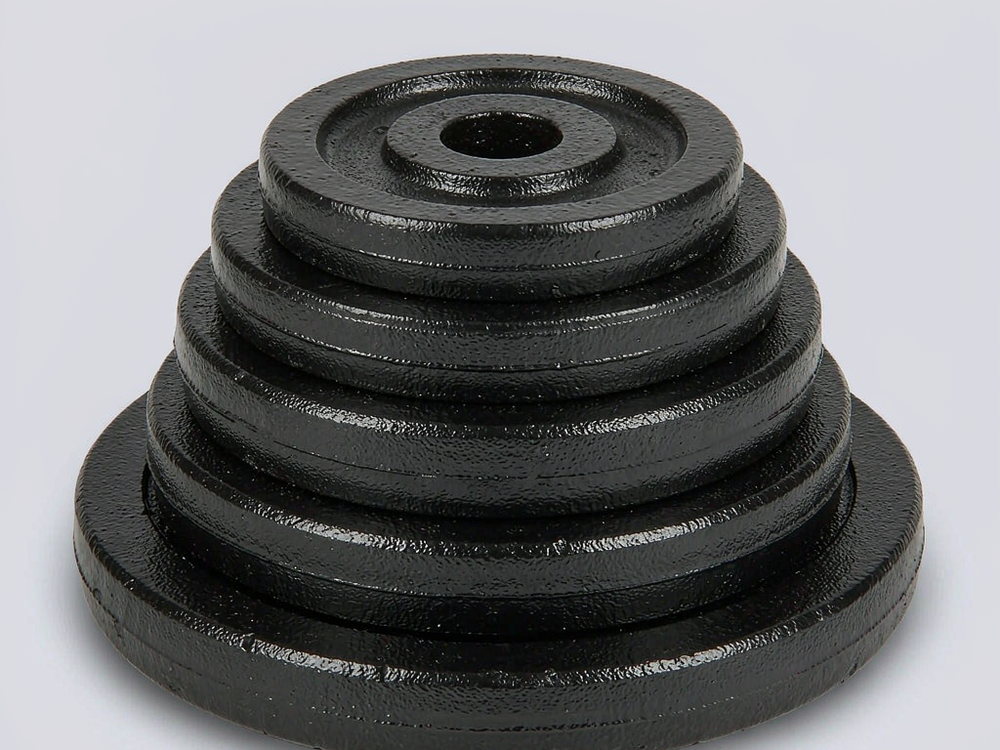
Stack of five cast iron barbell plates of decreasing diameter
Barbell plates1.25–25 kg · machined centre hole
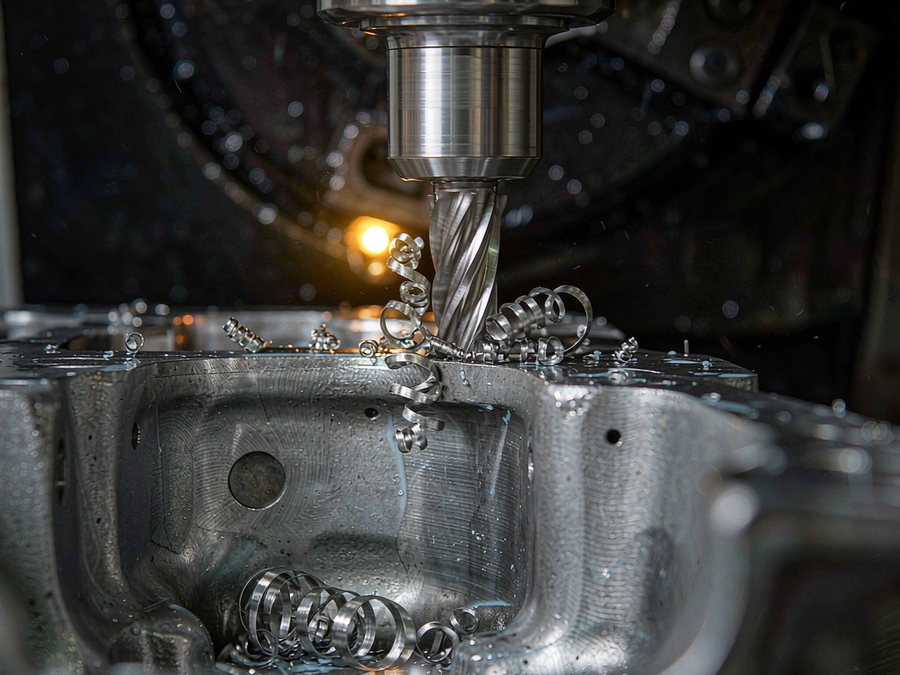
CNC end mill cutting a cast iron part with steel chips curling away
MachiningCored casting on a CNC fixture
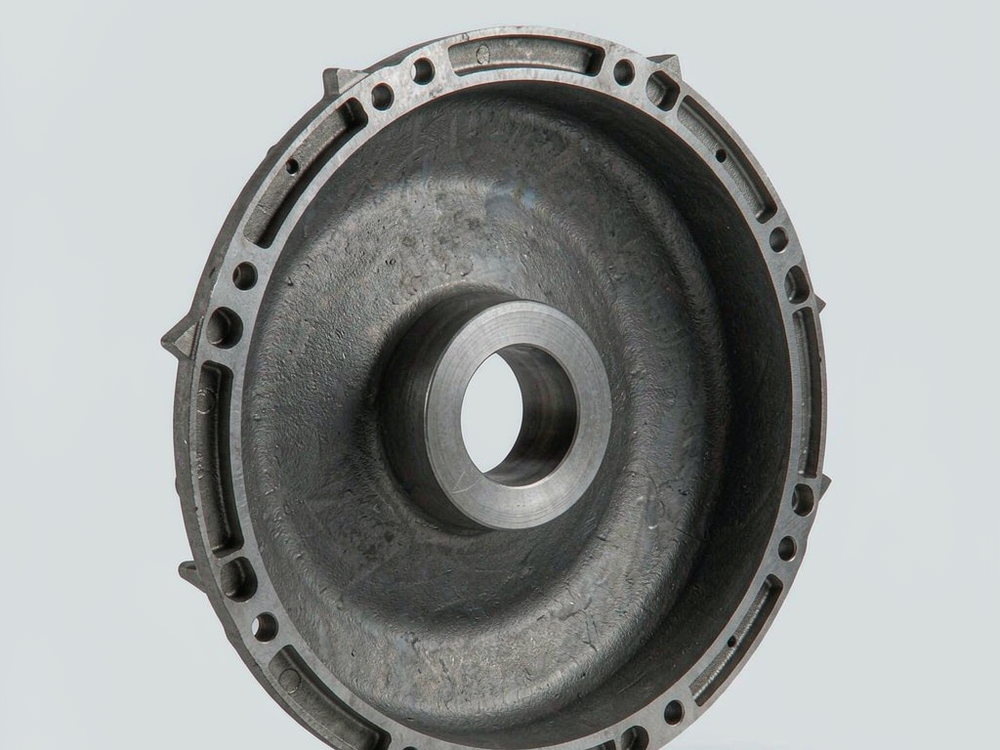
Round motor end cover casting with a ring of bolt holes and a central bearing boss
Motor end coverBearing seat and bolt circle
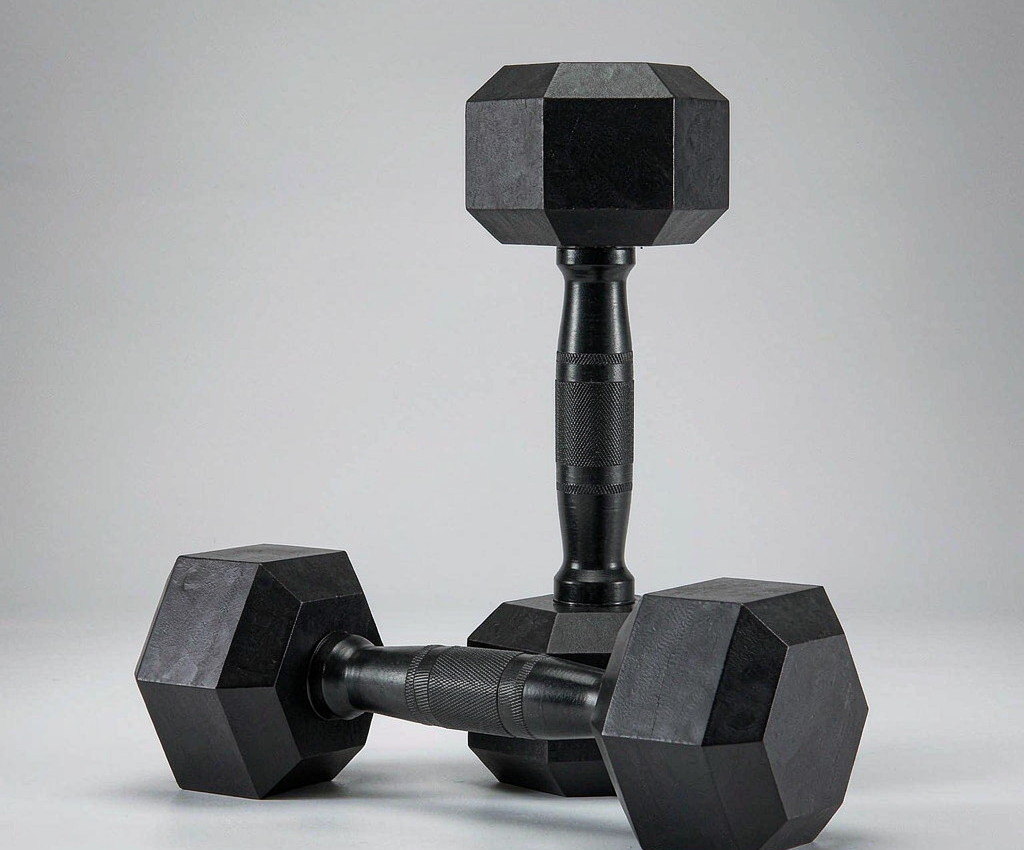
Hexagonal head dumbbells with diamond-knurled steel handles
Hex dumbbellsKnurled steel handle · six flat faces
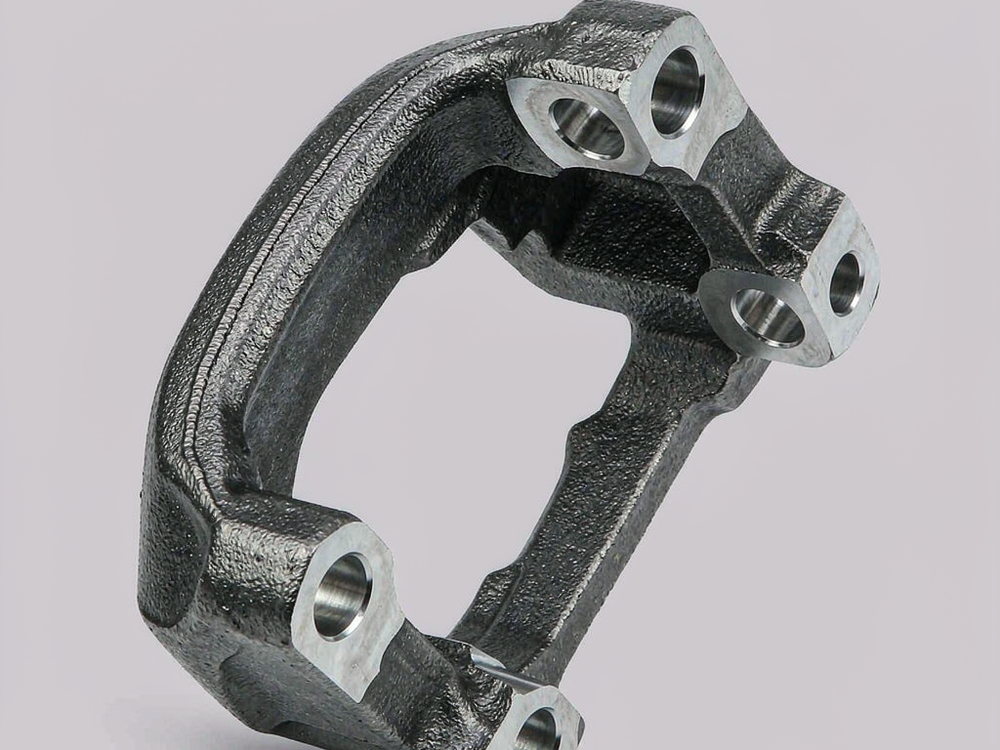
Curved ductile iron caliper bracket with two machined through bores
Caliper bracketDuctile iron · two slide-pin bores
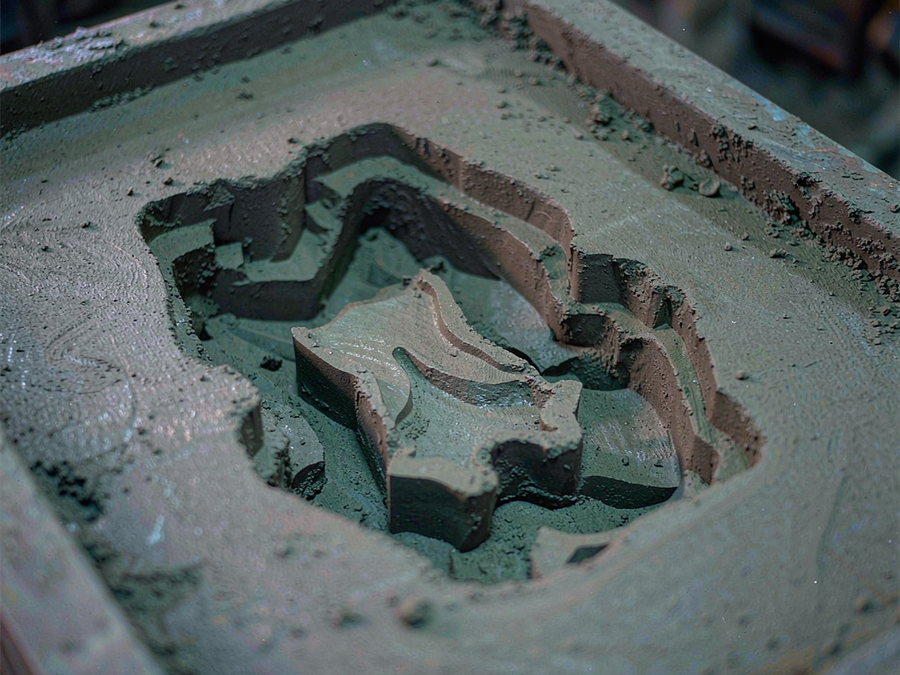
Green sand mould with a shell core located inside the cavity
Green-sand mouldShell core located before closing
Row of five competition kettlebells in different colours but the same body size
Competition kettlebellsColour-coded · one body size
As-cast iron body with cored internal passages before machining
As-cast bodyCored passages, before machining
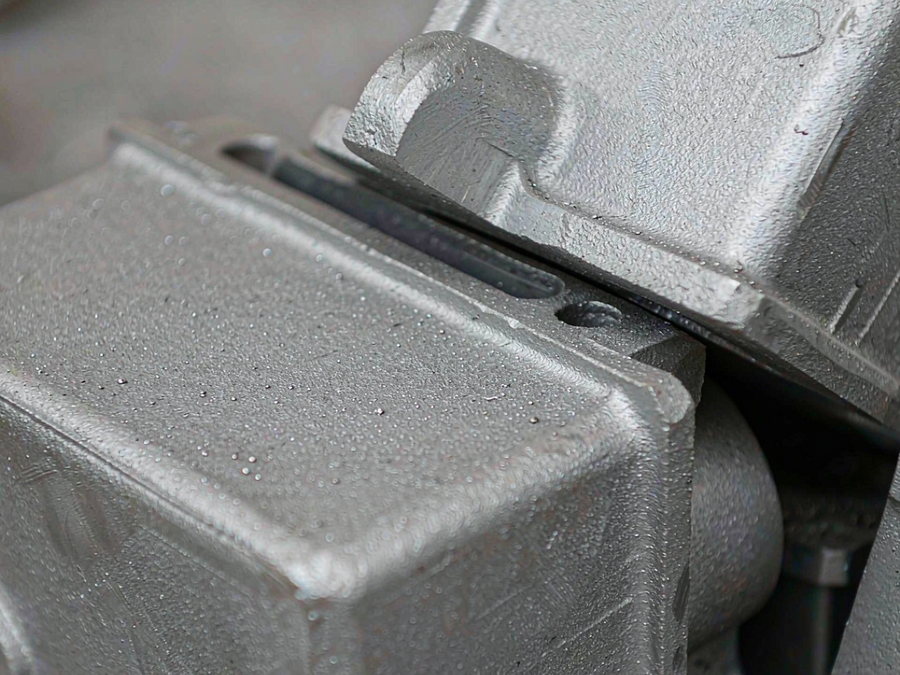
Shot-blasted grey iron castings with a uniform matte silver surface
After shot blastingUniform surface before inspection
Machined automotive casting from current production
Production castingFrom a current automotive programme
Round-head dumbbell pair with a smooth coated finish
Urethane optionRubber or PU on the same core

Product and process images are representative of the ranges we produce. Ask for a specific part number or weight and we will send that exact item, with its inspection record.

Full gallery →
Process

Six steps. We own five of them.

Surface finishing is the one step that leaves our floor — powder coating, e-coating and rubber or PU coating run through a fixed, qualified partner. We put that in writing because an auditor will find it anyway, and because a supplier who claims to do everything usually does nothing well.

Molten iron surface with a bright crust forming
01 — MeltMedium-frequency furnaces, spectrum analysis and inoculation control on every heat.
Sand mould cavity with a core in position
02 — MouldGreen-sand moulding on a DISA line; shell cores set by hand before closing.
End mill cutting into a cast iron casting
04 — MachineTurning, milling, grinding and CNC in the second plant, fixtures per part number.
Castings after shot blasting with a matte silver surface
03 — CleanShakeout, shot blast, gates and risers cut, burrs taken off by hand.
01

Melting & analysis

Every heat gets a number, a spectrum reading and a record that ships with the batch. Inoculation is controlled, not estimated.

02

Moulding

DISA automatic line for repeat volume, plus shell cores for internal passages. Patterns and core boxes are kept under the part number.

03

Cleaning & dressing

Shakeout, shot blasting, gate and riser removal. Edges a customer actually touches are deburred by hand, not by hope.

04

Machining

Sixty-five machining units in the second plant. Fixtures are built per part number so the second batch matches the first.

05

Inspection

Spectrum, hardness, dimensional checks and coordinate measuring. First-article report signed before any volume release.

06

Finishing · partner

Powder coating, e-coating, rubber and PU coating through a fixed qualified supplier. Adhesion and salt-spray reports filed per batch.

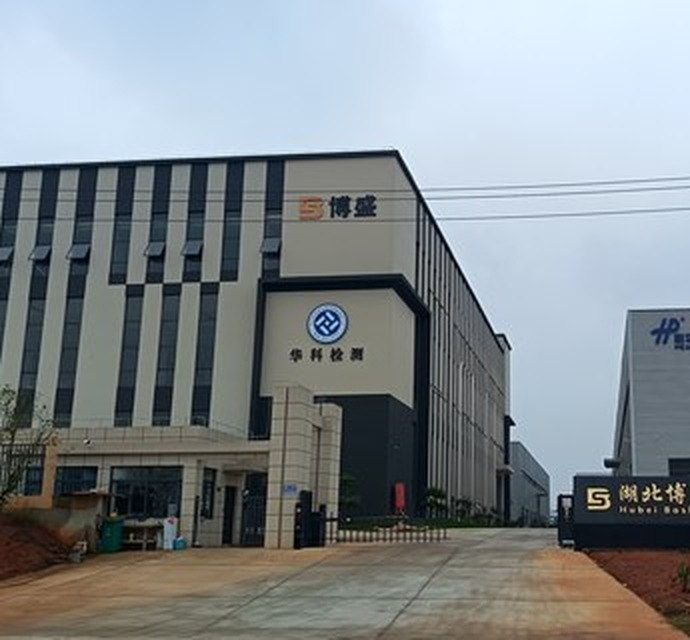
Bosheng plant building and yard in Xianning, Hubei
Machining plant, Fenghuang park. 20,000 m² on own land, 65 machining units, fifteen minutes from the foundry.
Two sites

Cast in Xiangyanghu.
Machined in Fenghuang.
Shipped as one.

The foundry sits in Xiangyanghu, the machining plant in the Fenghuang industrial park — both inside Xianning, both under the same ownership. When a bore drifts you call one number, not the foundry, then the machine shop, then whoever sold you the job.

20,000m²
Foundry site · 30 mu
260+65
Equipment sets
Plant details →
Scope

What we take on — and what we don't.

A supplier who says yes to everything is telling you nothing. Aluminium die casting, complex tooling and in-house heat treatment are outside our floor; sending those enquiries elsewhere saves us both a week.

Category Typical parts Status
Free weightsKettlebells (classic / competition), dumbbells, barbell platesIn production
Automotive castingsSteering housings, motor covers, reducer bodies, brake componentsIn production
Valve & pump bodiesGrey and ductile iron bodies, covers, flangesIn production
Industrial counterweightsMachine-tool weights, forklift and construction ballastIn production
Aluminium die casting—Not available
In-house heat treatment—Outsourced
Precision mould making—Outsourced
Quality

Nothing ships on a promise.

A new part number does not go to volume until the first article is measured and signed. For free weights that means a full-dimension report and weight sorted piece by piece; for machined parts, a CMM print with the critical bores called out.

Tolerance

Kettlebell weight within ±2% (competition ±1.5%); bores held to ±0.005 mm. Written into the spec sheet, not described as "high precision".

Traceability

Heat number, inspection record and packing list travel with the shipment. Give us a batch code and we can pull its file.

Quality system →
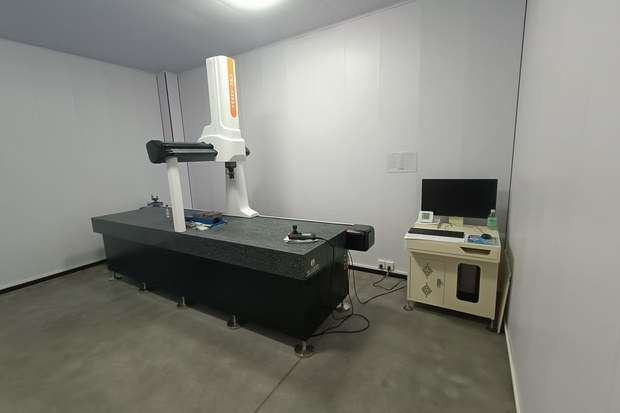
Coordinate measuring machine room used for first-article inspection
Coordinate measuring room. First-article reports are issued from here for every new part number — castings and free weights alike.
Next step

Send a drawing or a weight range. We answer with a process note, not a brochure.

A photo of the part, a PDF drawing, or just the weight and finish you need — enough for us to come back with routing, tooling cost and a lead time. Both lines go through the same inbox.